Selecting the right perforated screen is rarely about the simplest hole pattern; it is about managing the delicate balance between open area, structural integrity, and fluid dynamics. In high-precision industrial separation, a minor deviation in slot width or material grade can lead to catastrophic blinding or premature mechanical failure.
For engineers in the pharmaceutical, chemical, and mining sectors, the screen is the primary barrier that determines the purity of the final product. Whether dealing with aggressive mineral acids or sterile API crystallization, the technical requirements for these components demand more than just standard punching—they require advanced metallurgy and precision fabrication.
This analysis explores the critical technical variables and material selection strategies required to optimize filtration efficiency, focusing on how precision-engineered screens can resolve common operational bottlenecks in industrial centrifugation and separation processes.

Technical Foundations of Perforated Screening Systems

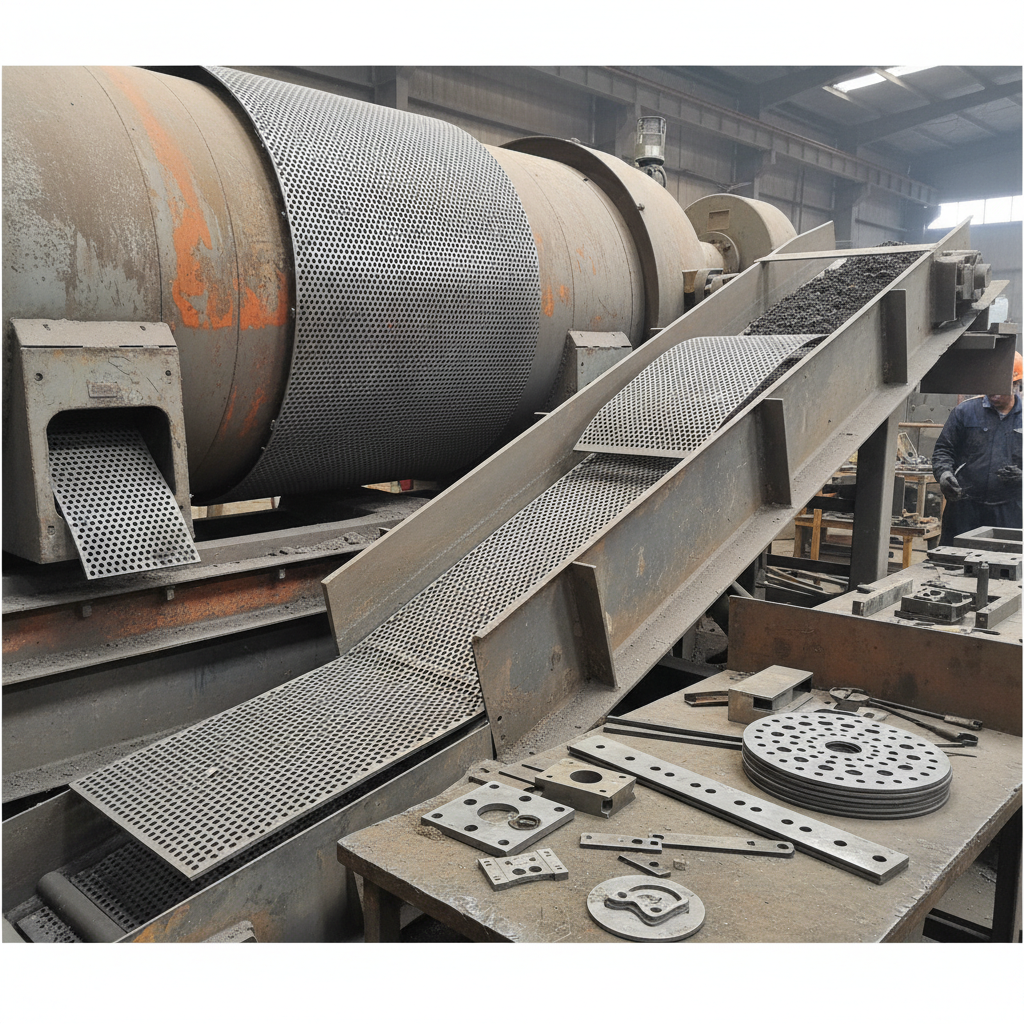
At its core, a perforated screen operates on the principle of size exclusion, but the industrial reality is far more complex than a simple sieve. The interaction between the particulate load and the screen surface is governed by the "open area" percentage and the precision of the slot width, which directly influence the pressure drop across the system.
In advanced configurations, such as the V-shaped wedge wire profile, the design is specifically engineered to be non-blinding. By creating a tapered aperture, particles are encouraged to pass through rather than wedge themselves into the opening, which is essential for maintaining a steady flow under high G-forces in centrifuge baskets.
The manufacturing process—ranging from traditional punching to precision laser welding—defines the tolerance of these apertures. For nanoparticle classification or high-purity API production, a tolerance of ±0.02 mm is often the difference between a successful batch and a rejected one.
Critical Material Selection for Harsh Environments
Material failure in screening systems usually stems from three sources: chloride-induced pitting, abrasive wear, or stress corrosion cracking. Selecting the correct alloy is not merely a cost consideration but a safety and uptime imperative.
For pharmaceutical environments, 316L or 904L stainless steel remains the benchmark due to its corrosion resistance and compatibility with electropolishing. Achieving a surface roughness of Ra ≤0.1 µm is critical for GMP compliance, ensuring that no biological residues remain trapped in surface micro-pores.
In contrast, mining applications requiring the processing of copper concentrates or kaolin clay demand extreme hardness. Plasma nitriding can elevate surface hardness up to 1,200 HV, effectively mitigating the erosive effects of high-velocity mineral slurries that would otherwise scour through standard stainless steel in weeks.
High-Impact Applications Across Global Industries
The versatility of precision perforated screens allows them to function in environments ranging from cryogenic biotech labs to hot asphalt centrifugation plants. Each application demands a specific geometry and material pairing to optimize the separation cycle.
In the food and beverage industry, specifically in palm oil refining or brewery yeast separation, the focus is on hygiene and flow. 904L stainless steel baskets with 0.2mm to 0.5mm slots are frequently employed to meet 3-A Sanitary Standards while maximizing the throughput of edible oils.
Within waste management and plastic recycling, the priority shifts to abrasion resistance and slot size. For PET flake purification, baskets with 3mm slots made from reinforced alloys are used to handle the high mechanical impact of recycled plastics, ensuring that only the desired particle size progresses through the line.
Evaluating Throughput and Separation Efficiency
Efficiency in screening is measured by the relationship between the open area and the retention rate. A screen with a 15–50% open area can maximize throughput while still retaining over 99% of particles within a specific micron range, provided the slot consistency is maintained.
When comparing standard perforated plates to precision wedge wire screens, the difference in "blinding resistance" becomes evident. The V-profile reduces the probability of particles becoming trapped, which maintains a more consistent flow rate over the duration of a production cycle.
perforated screen Performance Metrics
The data suggests that precision-engineered screens significantly reduce downtime caused by cleaning cycles. By optimizing the slot geometry and surface finish, plants can achieve a higher "uptime-to-cleaning" ratio, directly impacting the total cost of ownership.
Operational Best Practices for Screen Longevity
Extending the life of a screening system requires a holistic approach to maintenance, starting with the installation phase. For high-speed centrifuge baskets, dynamic balancing to a G2.5 grade is non-negotiable to prevent vibrational fatigue.
Regular inspection for "slot widening" is critical. In abrasive environments, the apertures can slowly enlarge, leading to a loss of separation precision. Implementing a scheduled passivation or electropolishing refresh can help maintain the hygienic properties and corrosion resistance of the surface.
Operators should also monitor the pressure differential across the screen. A sudden spike usually indicates the onset of blinding, suggesting that the cleaning frequency needs adjustment or that the material consistency has shifted beyond the screen's design parameters.
Emerging Trends in Filtration Geometry
The industry is moving toward "adaptive filtration," where screen geometries are customized based on the specific rheology of the material being processed. We are seeing a rise in helical and axial slot orientations to handle sticky materials like polymers or starch.
New material composites and advanced coatings, such as specialized plasma-sprayed ceramics, are likely to further increase the lifespan of screens in extremely corrosive mineral acid environments. This could potentially reduce the frequency of component replacement in sulfuric acid recovery systems.
Furthermore, the integration of laser welding has allowed for tighter tolerances (≤0.05 mm weld deviation), enabling the creation of larger diameter baskets (up to 2,000 mm) that remain stable under unbalanced load conditions, increasing the capacity of continuous centrifuges.
Comparative Framework for Screen Procurement
When procuring a new screening system, engineers must look beyond the initial price point and evaluate the Total Cost of Ownership (TCO). This involves analyzing the material grade against the chemical profile of the process fluid.
The following framework compares common screening approaches based on typical industrial requirements, helping procurement teams align the product specification with the operational reality.
| Solution Type | Primary Material | Key Strength | Ideal Use Case |
|---|---|---|---|
| Wedge Wire Screen | Duplex 2205 | Non-blinding flow | High-solids slurry |
| Precision Perforated | 316L Stainless | Sharp cut-points | Pharmaceutical API |
| Etched Metal Mesh | Hastelloy C-22 | Extreme corrosion resist | Acid purification |
| Expanded Metal | Carbon Steel (HDG) | Structural rigidity | Waste thickening |
| High-Hardness Screen | Nitrided Steel | Abrasion resistance | Kaolin clay processing |
| Biocompatible Mesh | Titanium Gr.2 | Zero toxicity | Cell harvesting |
Ultimately, the most cost-effective screen is the one that minimizes unplanned downtime. By aligning the metallurgy and geometry with the specific mechanical and chemical stresses of the application, facilities can ensure long-term operational stability.
Frequently Asked Questions
Conclusion
The efficiency of any industrial separation process is fundamentally limited by the performance of its screening components. By moving away from generic specifications and toward a precision-engineered approach—integrating advanced alloys like Duplex 2205 or Hastelloy with specialized geometries—operators can significantly reduce blinding and extend equipment life.
For those evaluating the technical requirements of their separation systems, detailed product specifications and material certifications can be found through www.tomaifilters.com, ensuring that the selected solution aligns with the rigorous demands of modern industrial manufacturing.